
How Specification-Driven Articles Improve Precision Measurement System Selection




How Specification-Driven Articles Improve Precision Measurement System Selection
For technical evaluators, selecting a precision measurement system requires more than comparing product features. It requires verified alignment between application requirements, measurable specifications, and operational constraints.
Specification-oriented articles precision measurement guidance helps teams translate tolerance, accuracy, repeatability, environmental conditions, and connectivity needs into defensible selection criteria.
When evaluation follows measurable specifications, organizations reduce procurement risk, improve inspection reliability, and choose metrology solutions that support long-term manufacturing performance rather than short-term purchasing convenience.
Search Intent: What Technical Evaluators Need to Decide
People searching for specification-driven guidance usually do not need a general explanation of metrology. They need a practical way to compare systems without overlooking critical technical limitations.
Their core intent is decision support. They want to know which specifications matter, how specifications interact, and how to distinguish meaningful capability from marketing language.
Technical evaluators often face competing claims from coordinate measuring machine, laser tracker, vision inspection, handheld scanner, caliper, gauge, and sensor suppliers.
A specification-oriented article provides a common comparison framework. It shifts discussion from product preference toward evidence, application fit, measurement uncertainty, and production consequences.
This approach is particularly valuable when systems will support critical dimensions, safety-related assemblies, regulated products, aerospace components, automotive parts, or high-value maintenance work.
The objective is not always to purchase the most accurate instrument. It is to select a system whose demonstrated capability matches the actual inspection task with appropriate margin.
Start With the Measurement Decision, Not the Instrument
The first question should be what decision the measurement result must support. A system used for process adjustment has different requirements than one used for final product acceptance.
Inspectors may need to confirm a single diameter, establish geometric compliance, monitor tool wear, align welded structures, verify assembly position, or create traceable digital records.
Each decision creates a different specification profile. A highly portable device may suit maintenance work, while a stable laboratory system may be necessary for tight geometric tolerances.
Define the part characteristic before reviewing equipment. Record nominal dimensions, tolerance limits, datum requirements, surface condition, material behavior, access restrictions, and measurement frequency.
This requirement definition prevents a common failure: selecting a measurement platform because it appears advanced, then discovering that it cannot reliably inspect the required feature.
It also prevents overinvestment. A sophisticated scanning system may offer exceptional visualization while delivering little additional value for a straightforward go or no-go inspection process.
Convert Drawing Requirements Into Evaluation Criteria
Technical drawings should become an evaluation checklist, not merely a final reference document. Identify all critical-to-quality features and rank them by manufacturing, safety, and customer risk.
For every critical feature, identify the required measurement method, access orientation, expected surface condition, measurement range, data output, and allowable uncertainty contribution.
Include form and positional requirements, not only linear dimensions. Flatness, concentricity, profile, runout, perpendicularity, and true position can demand fundamentally different measurement capabilities.
Where tolerances vary across a component family, evaluate the tightest credible production requirement. Buying against an average requirement can create a capability gap when product mix changes.
Accuracy Is Important, but It Is Not the Entire Selection Case
Accuracy is usually the first specification buyers compare, yet it is frequently misunderstood. Published accuracy may apply only under controlled conditions and specific measurement ranges.
System accuracy describes closeness to a reference value, but actual inspection confidence also depends on calibration, setup, operator technique, part condition, and measurement strategy.
A supplier may state maximum permissible error using a formula such as a fixed micrometer value plus a distance-dependent term. Evaluators must calculate performance at their working range.
For example, a system suitable for short-range fixture verification may become less appropriate when measuring large fabricated structures, long assemblies, or components across a production cell.
Do not compare accuracy figures without checking units, confidence assumptions, temperature conditions, artifact types, and whether the stated value represents system, probe, or software performance.
Ask suppliers for uncertainty budgets that show the main contributors. This makes it easier to identify whether environmental variation, fixturing, probing, or software alignment dominates the result.
Use a Practical Tolerance-to-Uncertainty Relationship
A useful selection principle is to maintain enough separation between product tolerance and measurement uncertainty. The required ratio depends on quality risk, customer requirements, and inspection consequences.
Many organizations use a measurement capability target such as a ten-to-one relationship, although lower ratios may be acceptable when supported by guard bands and risk analysis.
The correct rule is not universal. A cosmetic feature, a critical aircraft interface, and a high-volume automotive bore may require very different measurement decision controls.
Evaluate the complete measurement process, not only the instrument. A device with excellent stated accuracy can still yield poor results when part positioning is inconsistent.
Measurement system analysis, including repeatability and reproducibility studies, should validate the expected result before deployment. Purchase approval should not replace practical capability confirmation.
Repeatability and Reproducibility Determine Shop-Floor Confidence
Repeatability measures variation when the same operator measures the same feature repeatedly under consistent conditions. It matters because inspection decisions must remain stable over time.
Reproducibility measures variation among operators, setups, shifts, or locations. It is especially important when a system will move between production lines or global facilities.
A measurement system may produce an accurate reading once while still failing to support reliable production control. Technical evaluators should treat this as a serious operational risk.
Specification-driven articles precision measurement planning should therefore request evidence of repeatability using representative parts, surfaces, fixtures, probes, and operator workflows.
Consider whether measurements require manual alignment, feature extraction, probe changes, scanning paths, or interpretation of visual data. Every manual step can introduce reproducibility variation.
Automation may reduce some operator variation, but automated systems also require reliable fixturing, validated programs, maintained reference artifacts, and clear recovery procedures after faults.
Test the Workflow, Not Just the Demonstration
Supplier demonstrations often use clean samples, experienced application engineers, controlled lighting, and optimized measurement programs. These conditions may not represent normal manufacturing reality.
Request a proof-of-capability test using representative production parts whenever the purchase affects high-risk dimensions, expensive rework, customer acceptance, or regulated quality documentation.
Include common difficulties in the test, such as reflective surfaces, burrs, weld spatter, oil residue, difficult access, variable casting texture, or temperature differences.
Ask multiple intended users to participate. Their experience will reveal whether the interface, measurement sequence, reporting functions, and handling requirements are realistic for the operating environment.
Environmental Specifications Can Override Laboratory Performance
Precision measurement depends on physical conditions. Temperature, vibration, contamination, lighting, humidity, electromagnetic interference, and air movement can materially affect measurement results.
Laboratory-grade accuracy may be unnecessary or unattainable on a production floor. The important question is whether the system performs predictably in its intended operating environment.
Temperature deserves particular attention because both parts and instruments expand or contract. Large metal components may not reach thermal equilibrium before measurement begins.
Evaluate whether the system provides temperature compensation, what inputs it requires, and whether compensation assumptions match the material, part geometry, and actual production workflow.
For optical and vision-based systems, assess ambient lighting, surface reflectivity, contrast, transparency, and line-of-sight constraints. These factors can affect feature detection and scan completeness.
For contact systems, assess probe force, stylus access, fixture rigidity, dirt accumulation, surface damage risk, and the effect of compliant or thin-walled components.
Match Protection Ratings to Actual Exposure
Ingress protection, operating temperature range, shock resistance, and battery performance should be evaluated against real exposure rather than vague assumptions about shop-floor use.
A handheld instrument used near coolant, grinding dust, welding operations, or outdoor service work needs different protection than an instrument used in a controlled inspection room.
Document cleaning requirements and calibration stability after exposure. Maintenance effort is a specification consideration because neglected upkeep eventually becomes a measurement reliability problem.
Range, Access, and Throughput Must Work Together
Measurement range alone does not guarantee practical coverage. Evaluators should consider reachable volume, probe orientation, line of sight, part rotation, fixture clearance, and operator access.
A large-volume system may cover the part envelope but struggle with hidden features, deep bores, narrow gaps, internal geometries, or complex welded assemblies.
Conversely, a compact measuring device may provide excellent local accuracy while requiring excessive repositioning, multiple alignments, or complicated transfer procedures for larger components.
Throughput should be measured as total cycle time, including loading, fixturing, warm-up, program selection, alignment, measurement, report review, unloading, and exception handling.
Fast data capture is not always fast inspection. A scanner can acquire millions of points quickly, but processing, alignment, mesh handling, and report generation may extend the workflow.
For high-volume production, calculate the number of parts per shift, required sampling plan, operator availability, system uptime, and time needed for calibration verification.
Consider the Cost of Measurement Delays
When inspection becomes a bottleneck, production teams may bypass the approved process, reduce sampling discipline, or release parts before sufficient evidence is available.
These behaviors create more risk than an initially slower but well-integrated system. The selected solution must fit the pace and discipline of the manufacturing process.
Evaluate whether measurements can occur in-process, near-line, at-line, or offline. The best location depends on feedback speed, required accuracy, environmental control, and production interruption cost.
Connectivity and Data Integrity Are Part of Measurement Capability
Modern precision measurement systems increasingly connect with quality software, manufacturing execution systems, statistical process control platforms, and product lifecycle management environments.
Connectivity matters when teams need automated traceability, closed-loop process adjustment, revision control, remote review, customer reporting, or coordinated quality records across facilities.
Technical evaluators should verify supported file formats, application programming interfaces, network requirements, user permissions, audit trails, backup methods, and cybersecurity responsibilities.
A system that produces accurate data but creates isolated files may increase administrative work and weaken traceability. Manual transcription also creates avoidable opportunities for error.
Confirm whether reports can show nominal values, actual values, deviations, pass-or-fail status, measurement uncertainty, inspection plans, operator identification, and equipment calibration status.
For connected tools and intelligent torque systems, ensure measurement data can be associated with product serial numbers, assembly stages, work orders, and approved process parameters.
Protect Data Interpretation From Software Risk
Software functions should be evaluated as carefully as hardware specifications. Feature extraction, alignment algorithms, filtering settings, datum logic, and tolerance interpretation can change results.
Ask how software updates are qualified and whether legacy inspection programs remain valid. A measurement result is only defensible when the calculation path is controlled and understandable.
Require training on program validation, change management, access control, and report review. These controls are important when data supports customer claims or formal quality decisions.
Build a Defensible Supplier Comparison Matrix
A structured comparison matrix makes procurement discussions more objective. It should score systems against weighted requirements rather than relying on brochure summaries or anecdotal preferences.
Separate mandatory requirements from desirable capabilities. A system that fails a mandatory access, uncertainty, compliance, or environmental requirement should not remain competitive through optional features.
Common comparison categories include accuracy, repeatability, range, throughput, environmental suitability, automation, software, connectivity, calibration, service coverage, training, and total ownership cost.
Assign technical weights before reviewing supplier proposals. This reduces the chance that an impressive demonstration, familiar brand, or lower purchase price distorts the decision.
For each score, record supporting evidence. Acceptable evidence may include calibration certificates, performance tests, documented standards compliance, customer references, application studies, and verified workflow trials.
Use uncertainty ranges where evidence is incomplete. A supplier claim without supporting conditions should receive less confidence than a demonstrated result using representative parts and procedures.
Include Lifecycle Costs, Not Only Purchase Price
Total cost of ownership includes calibration, fixtures, probes, software licenses, maintenance, spare parts, training, validation, downtime, upgrades, and internal engineering support.
Lower-cost equipment can become expensive when it requires frequent specialist intervention, proprietary consumables, extended programming time, or shipment to distant calibration facilities.
Also consider business continuity. Review local service response, application engineering availability, replacement equipment options, warranty terms, and supplier stability in the relevant region.
Use Specification-Driven Content as an Internal Decision Tool
Well-structured specification-oriented articles precision measurement teams can use internally do more than educate readers. They create a repeatable language for engineering, quality, operations, and procurement.
Engineering teams can define product requirements. Quality teams can establish acceptance confidence. Operations teams can assess throughput. Procurement teams can compare commercial proposals without diluting technical priorities.
This shared framework is valuable in global manufacturing environments, where different sites may otherwise select incompatible tools, apply inconsistent inspection methods, or maintain fragmented quality records.
It also supports supplier communication. Instead of asking for the “best” system, evaluators can request a documented proposal against defined part characteristics, risks, conditions, and outputs.
For distributors and industrial decision makers, this method improves credibility. Recommendations become easier to justify because they are tied to measurable customer requirements rather than generalized product claims.
Conclusion: Select the System That Produces Reliable Decisions
The strongest precision measurement system selection process starts with the manufacturing decision, then translates that decision into measurable technical and operational requirements.
Accuracy remains essential, but repeatability, uncertainty, environment, access, throughput, connectivity, software control, and lifecycle support determine whether a system succeeds in daily use.
Specification-driven articles improve evaluation quality because they turn broad metrology discussions into practical selection criteria. They help technical evaluators ask better questions and demand stronger evidence.
The final choice should be the system that delivers reliable, traceable, repeatable information at the required speed and cost within the actual conditions of production.
Related News
How Procurement Teams Can Map the Industrial Value Chain to Reduce Supply Risk
Industrial value chain procurement helps teams map hidden dependencies, qualify resilient sources, and reduce supply risk before disruptions stop production.
How to Evaluate a Technology Integration Service Provider for Complex Projects
Technology integration service provider selection guide: evaluate interface ownership, delivery discipline, scalable architecture, and risk control for complex projects.
How Battery, Torque, and Duty Cycle Affect Cordless Power Tool Efficiency
Cordless power tool efficiency depends on battery output, torque, and duty cycle. Learn how to match tools to demanding jobs for stronger runtime and productivity.
Product Comparison Resources for Component Compatibility and Lifecycle Risk
Product comparison resources for components: evaluate compatibility, interfaces, service support, and lifecycle risk to reduce downtime, avoid redesigns, and make confident sourcing decisions.
How to Select Vernier Precision Calipers for Tight-Tolerance Machining Inspection
Vernier precision calipers for tight-tolerance machining: learn how to select the right range, jaw design, accuracy, and verification process for reliable inspection.
Product Comparison Resources in Europe: How Buyers Can Verify Specs and Suppliers
Product comparison resources Europe: learn how to verify industrial specs, compliance claims, supplier credibility, and delivery risk for smarter purchasing decisions.
How to Evaluate an Industrial Metrology Solution Manufacturer for Production Use
Industrial metrology solution manufacturer evaluation guide for production: compare accuracy, traceability, automation, software, service, and acceptance testing to reduce risk.
Which ISO Standards Matter Most for Precision Engineering Quality Control?
Precision engineering ISO standards explained: discover how ISO 9001, ISO/IEC 17025, ISO 10012, GPS, and ISO 3834 strengthen quality control, traceability, and compliance.
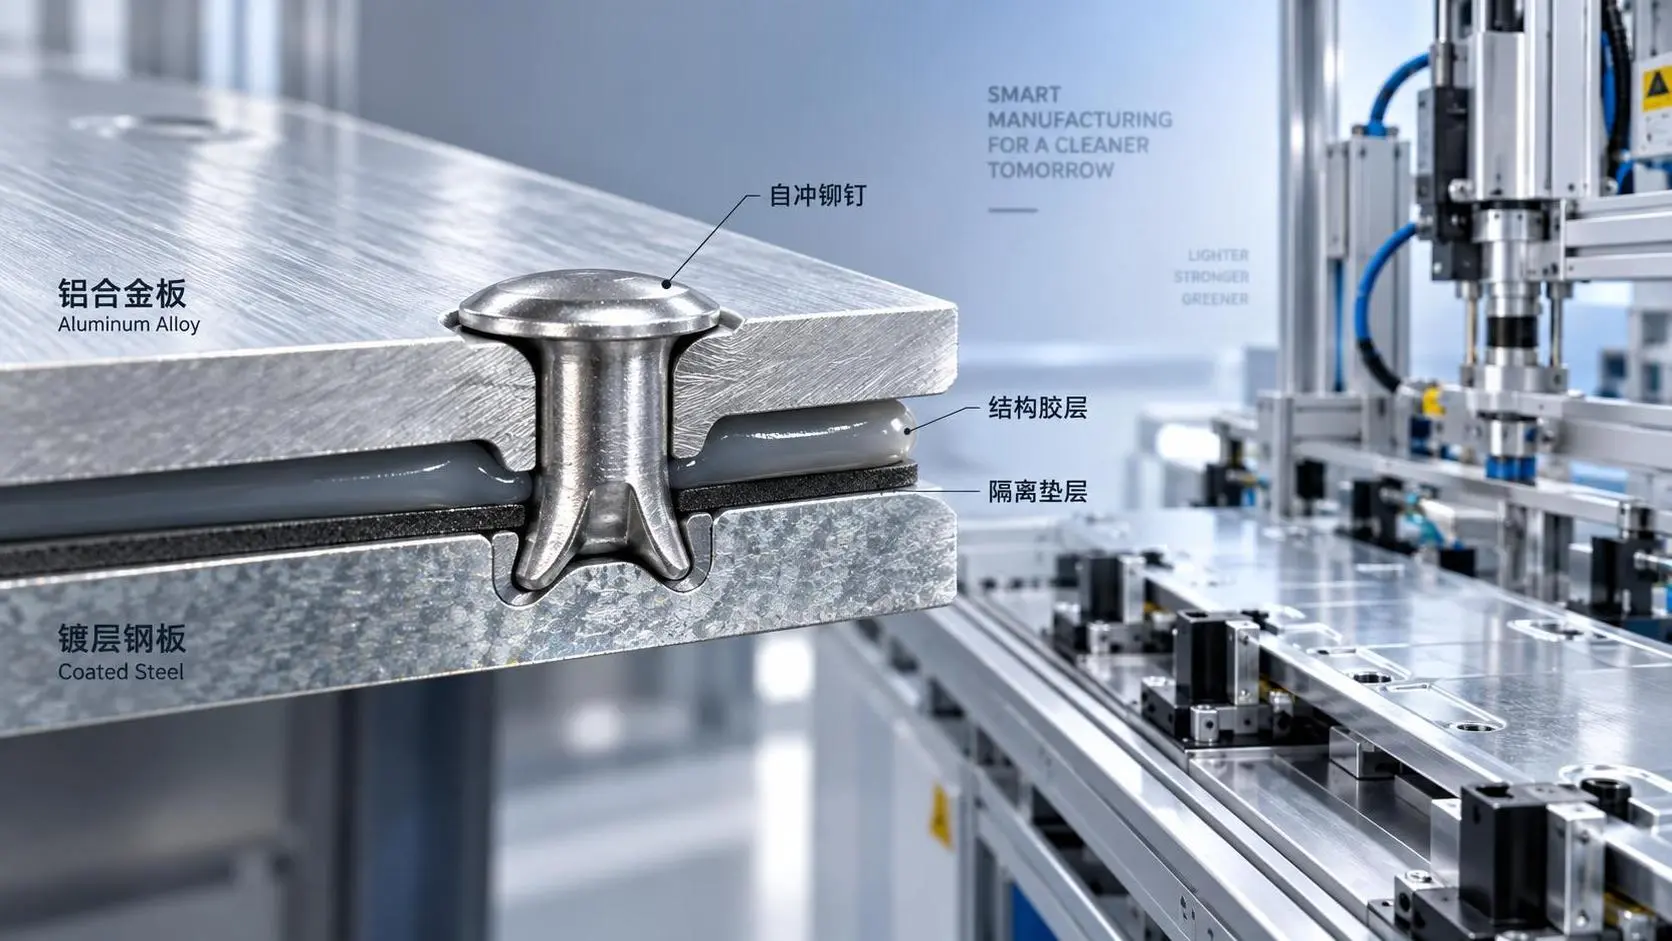
Selecting Metal Joining Methods for Aluminum-to-Steel Assemblies
Metal joining solutions for dissimilar metals: compare aluminum-to-steel fastening, bonding, hybrid, and thermal methods for corrosion-resistant, reliable assemblies.
Related News
- 00
0000-00
How Specification-Driven Articles Improve Precision Measurement System Selection - 00
0000-00
Product Comparison Resources for Component Compatibility and Lifecycle Risk - 00
0000-00
Which ISO Standards Matter Most for Precision Engineering Quality Control? - 00
0000-00
Selecting Metal Joining Methods for Aluminum-to-Steel Assemblies - 00
0000-00
How to Evaluate Industrial Manufacturing Systems for Throughput, Flexibility, and ROI
Prof. Marcus Chen
Weekly Insights
Stay ahead with our curated technology reports delivered every Monday.