
How Procurement Teams Can Map the Industrial Value Chain to Reduce Supply Risk




A late delivery of a welding power source, a sudden export control on an electronic drive, or a batch of calipers that fails repeatability checks can interrupt production far beyond the value of the individual purchase order. For procurement teams, the issue is rarely one supplier in isolation. It is the network behind that supplier: mills, forgings, motor manufacturers, electronics assemblers, calibration labs, freight corridors, and the standards that connect them.
Industrial value chain procurement gives buyers a way to see that network before it becomes a crisis. Rather than treating a sourcing decision as a comparison of unit prices and lead times, value-chain mapping reveals where a component truly originates, which technical dependencies are difficult to replace, and where alternative supply is real rather than merely listed in a supplier database.
This matters especially in the “last mile” of manufacturing: industrial assembly, metal joining, precision tools, and metrology. A production line may have substitute options for a general fastener, yet no easy replacement for a torque-control controller, a certified welding consumable, a precision spindle, or a measurement instrument tied to an established quality system. The risk is not only supply interruption. It can also be hidden loss of accuracy, operator safety exposure, requalification costs, and delayed customer shipments.
Begin with the part that would hurt most to lose
Many mapping efforts fail because they begin too broadly. Teams attempt to diagram every supplier, every category, and every shipment route at once. The result is often a large but static chart that does not guide decisions.
A more useful starting point is the “production stopper” question: Which purchased item would halt output, compromise a critical quality requirement, or force an expensive revalidation if it became unavailable? The answer is not always the highest-spend item.
In an industrial tools and joining environment, critical items often include:
- Brushless motors, controllers, switches, and battery-management components for cordless or automated tools;
- Precision gears, bearings, chucks, hydraulic seals, and machined housings with narrow tolerance requirements;
- Laser sources, optics, wire feeders, shielding-gas control parts, and safety-related equipment for welding systems;
- Calipers, micrometers, torque analyzers, gauges, sensors, and calibration services that support quality release;
- Specialty steel grades, copper alloys, abrasives, fluxes, electrodes, and other material inputs whose performance depends on composition and process control;
- Software, firmware, and connectivity modules used in IoT-enabled torque or traceability systems.
Assign every critical item a concise business consequence statement. “Long lead time” is not enough. A stronger statement might read: “Loss of this encoder supplier would stop final assembly within the existing buffer window; alternative units require electrical and accuracy validation.” This wording makes technical risk visible to commercial stakeholders and gives engineering a clear reason to participate.
Map the chain in layers, not as a supplier list
A tier-one supplier name is only the front door. To reduce supply risk, procurement needs a layered view that follows the physical product, the technical specification, and the route to market.
Layer 1: The purchased item and its operating requirement
Document the exact item being bought: drawing revision, material or performance specification, approved standards, inspection method, packaging requirement, and expected service environment. For a welding torch, this could include duty cycle, consumable interface, cable configuration, and heat resistance. For a digital torque tool, it may include range, accuracy, data protocol, battery architecture, and traceability needs.
This layer prevents a common mistake: assuming two catalog descriptions represent equivalent supply. They may look interchangeable until one fails to communicate with a production system, withstand shop-floor conditions, or satisfy the measurement uncertainty required by the customer.
Layer 2: Direct supply and site-level exposure
Capture more than the legal supplier entity. Identify the manufacturing location, final assembly site, warehouse location, and service or calibration center. A supplier with offices in several countries may still manufacture a critical product family at one facility. Likewise, two approved distributors may draw inventory from the same regional hub.
At this stage, buyers should ask whether the supplier is producing, assembling, stocking, or simply reselling. Each role creates different exposure. A distributor can provide valuable local availability, but it does not automatically create manufacturing redundancy.
Layer 3: Subcomponents, raw materials, and process bottlenecks
This is where the industrial value chain becomes most revealing. Request a practical bill-of-materials view for priority items, focusing on components that are proprietary, regulated, difficult to machine, or dependent on specialized processing. The goal is not to demand every supplier’s confidential commercial detail. It is to understand concentration and constraint.
For example, a handheld laser welding system may depend on a small number of laser-source manufacturers, optical components, control electronics, and safety interlocks. A precision measuring instrument may rely on a scale technology, sensor chip, hardened guideway, or calibration reference that cannot be quickly duplicated. A power tool’s nominally simple motor may depend on magnets, copper winding capacity, electronics, and specialized balancing equipment.
Material sourcing deserves equal attention. A forged steel body and a machined aluminum housing may have different exposure to regional capacity, energy costs, trade measures, and alloy availability. The direct supplier may appear stable while its material source is the actual bottleneck.
Layer 4: Standards, approvals, and knowledge dependencies
Not every dependency travels in a container. Some are embedded in technical approvals, test methods, proprietary firmware, operator training, or calibration capability. If a replacement supplier can make a similar part but cannot provide the required documentation, measurement traceability, welding procedure support, or safety evidence, the practical supply option may be unusable.
For procurement, this layer is often the difference between “we have a backup source” and “we have a qualified backup source.” Record the approval owner, validation steps, typical requalification duration, required samples, and any customer-specific restrictions.
Layer 5: Logistics, trade, and market access
Finally, map how the product moves: port or border crossing, inland carrier, customs classification, export restrictions, dangerous-goods handling, insurance requirements, and the inventory point at which ownership or risk transfers. A supply chain can be geographically diversified yet still depend on one airport lane, one port, or one export licensing process.
For equipment containing electronics, lasers, batteries, or controlled technology, trade and documentation checks should be part of routine sourcing—not an emergency exercise after an order has been placed.
Turn the map into a decision tool
A value-chain map becomes useful when it helps buyers decide where to spend time and money. One practical approach is to score critical categories against several dimensions rather than relying on a single “risk level.”
Use a simple scoring model if it helps prioritize, but do not let the score replace judgment. A component with moderate spend and high requalification burden may deserve more attention than a high-spend item purchased from several genuinely independent and technically approved sources.
Separate dual sourcing from meaningful resilience
“We have two suppliers” is one of the most comforting—and potentially misleading—statements in procurement. Two suppliers do not create resilience if they buy the same subcomponent, manufacture in the same industrial cluster, rely on the same logistics route, or use the same licensed technology.
Meaningful dual sourcing has independence at the point of constraint. For a critical welding consumable, that may mean separate manufacturing and wire-drawing capability. For an electronic torque controller, it may mean different design and component supply paths, not simply different labels on a common board. For metrology equipment, it may require separate repair and calibration channels that can maintain the required measurement confidence.
There is also a commercial side. Buyers should understand capacity allocation rules, minimum order quantities, lead-time commitments, tooling ownership, and the supplier’s ability to support demand spikes. A second source that only accepts small spot orders will not protect a production ramp.
That does not mean every category needs full dual sourcing. The cost of qualification may outweigh the benefit for some specialized equipment. In those cases, resilience may come from strategic spare units, repair agreements, carefully sized inventory, access to loan equipment, or contractual visibility into the supplier’s own continuity plans.
Build technical teams into the procurement workflow early
Supply risk is often discovered late because commercial discussions and technical decisions occur on separate tracks. Procurement sees a price increase or extended lead time; engineering sees a change request; quality sees a failed incoming inspection. By the time those signals meet, the organization is reacting under pressure.
A cross-functional review for high-risk categories should be short, recurring, and specific. Procurement brings supplier intelligence, capacity signals, and contract status. Engineering explains functional interchangeability and redesign exposure. Quality clarifies inspection and approval requirements. Operations identifies actual buffer consumption and production impact. Logistics contributes route and trade visibility.
For precision tools and metrology, involve the people responsible for calibration and process capability. A measurement device is not simply an MRO purchase when it is used to accept product, verify torque, or support regulated documentation. Its availability, service intervals, software compatibility, and reference standards belong on the risk map.
Watch the signals that appear before a shortage
The most valuable intelligence is often not a dramatic announcement. It is a pattern of smaller changes: repeated delivery-date movement, unusual requests for blanket orders, a supplier shifting from standard lead time to “subject to allocation,” a revised country of origin, or a sudden restriction on technical documentation.
For industrial value chain procurement, maintain a focused watchlist around the categories that matter most. Useful signals include raw-material volatility, changes in export standards or customs requirements, factory consolidation, workforce constraints in specialist trades, new safety expectations for handheld laser welding, and demand shifts in construction, automotive maintenance, aerospace repair, or industrial automation.
GPTWM’s Strategic Intelligence Center follows many of these connections across metal joining, industrial assembly, hydraulic equipment, power tools, and precision measurement. For buyers, the practical value of sector intelligence is not another headline. It is the ability to connect an external development—such as a material constraint, evolving welding safety expectation, or shift in brushless-motor demand—to a named category in the sourcing plan.
Make the map part of sourcing, not a crisis document
A value-chain map should change what happens before an RFQ is issued. Include origin transparency, sub-tier concentration, continuity planning, repair capacity, and change-notification expectations in supplier conversations. Ask prospective suppliers which inputs have the longest replenishment cycle, what alternatives they have qualified, and which specifications would be hardest to maintain during disruption.
During negotiations, procurement can also use the map to distinguish where cost reduction is sensible from where it is dangerous. Consolidating spend may improve price and administration in a low-risk category. In a technically constrained category, however, over-consolidation can create a dependency that costs far more than the savings when supply falters.
Review the map when something changes: a new product launch, a design revision, a supplier acquisition, a shift in manufacturing location, a new customer requirement, or a material market event. The document does not need to be perfect to be valuable. It needs to remain connected to actual purchasing decisions.
A clearer view creates calmer decisions
Procurement teams cannot eliminate every disruption. They can, however, reduce surprises by understanding where industrial products are made, what makes them technically difficult to replace, and which hidden links connect seemingly separate suppliers.
That perspective turns supply risk from an abstract dashboard metric into a manageable set of choices: qualify another source, protect inventory, revise a specification, secure service coverage, redesign selectively, or accept a known exposure with eyes open. In industries where welding quality, assembly reliability, and measurement accuracy shape the final product, that clarity protects more than purchasing performance. It protects the confidence of the factory floor and the promises made to customers.
Related News
How Specification-Driven Articles Improve Precision Measurement System Selection
Specification-oriented articles precision measurement guidance helps teams compare accuracy, repeatability, environment, and data needs to select reliable systems with confidence.
How to Evaluate a Technology Integration Service Provider for Complex Projects
Technology integration service provider selection guide: evaluate interface ownership, delivery discipline, scalable architecture, and risk control for complex projects.
How Battery, Torque, and Duty Cycle Affect Cordless Power Tool Efficiency
Cordless power tool efficiency depends on battery output, torque, and duty cycle. Learn how to match tools to demanding jobs for stronger runtime and productivity.
Product Comparison Resources for Component Compatibility and Lifecycle Risk
Product comparison resources for components: evaluate compatibility, interfaces, service support, and lifecycle risk to reduce downtime, avoid redesigns, and make confident sourcing decisions.
How to Select Vernier Precision Calipers for Tight-Tolerance Machining Inspection
Vernier precision calipers for tight-tolerance machining: learn how to select the right range, jaw design, accuracy, and verification process for reliable inspection.
Product Comparison Resources in Europe: How Buyers Can Verify Specs and Suppliers
Product comparison resources Europe: learn how to verify industrial specs, compliance claims, supplier credibility, and delivery risk for smarter purchasing decisions.
How to Evaluate an Industrial Metrology Solution Manufacturer for Production Use
Industrial metrology solution manufacturer evaluation guide for production: compare accuracy, traceability, automation, software, service, and acceptance testing to reduce risk.
Which ISO Standards Matter Most for Precision Engineering Quality Control?
Precision engineering ISO standards explained: discover how ISO 9001, ISO/IEC 17025, ISO 10012, GPS, and ISO 3834 strengthen quality control, traceability, and compliance.
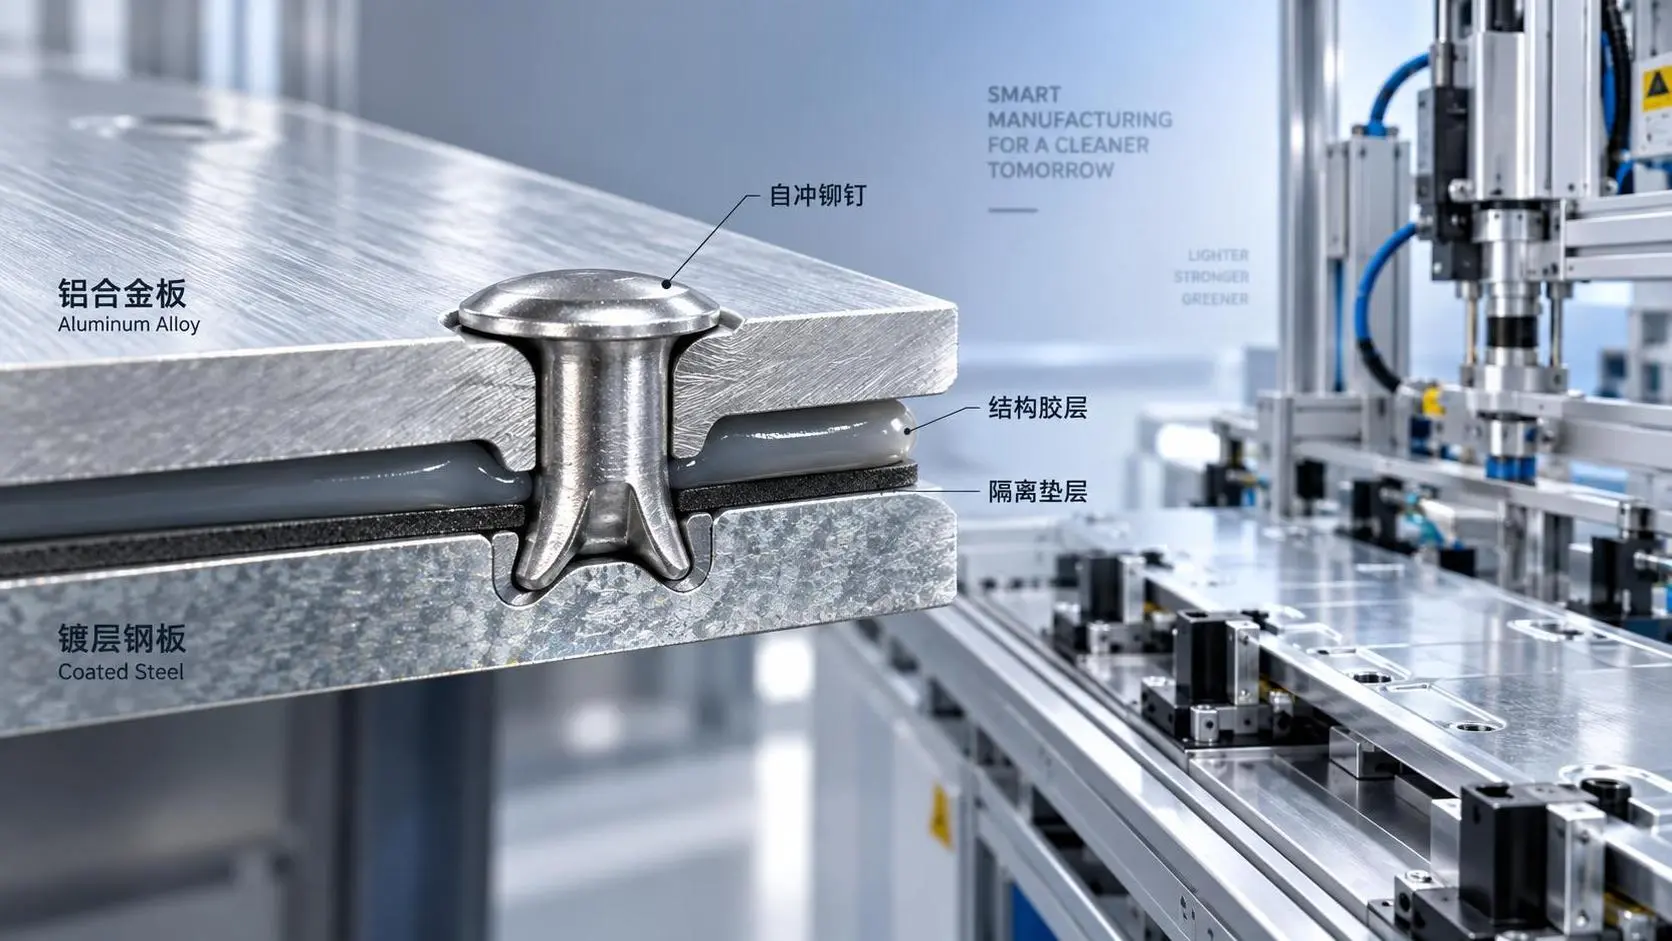
Selecting Metal Joining Methods for Aluminum-to-Steel Assemblies
Metal joining solutions for dissimilar metals: compare aluminum-to-steel fastening, bonding, hybrid, and thermal methods for corrosion-resistant, reliable assemblies.
Related News
- 00
0000-00
How Procurement Teams Can Map the Industrial Value Chain to Reduce Supply Risk - 00
0000-00
How Industry Category Guides Help Global Sourcing Teams Compare Suppliers Faster - 00
0000-00
Intelligent Tools in Southeast Asia: Key Market Trends, Buyers, and Supply Chain Shifts - 00
0000-00
Industrial Value Chain Europe: Where Sourcing Risks and Lead-Time Pressure Are Rising - 00
0000-00
North America's Industrial Value Chain: Key Shifts in Sourcing, Labor, and Logistics
Dr. Alistair Vaughn
Weekly Insights
Stay ahead with our curated technology reports delivered every Monday.