
How Material Science Affects Weld Strength, Distortion, and Heat-Affected Zones




Weld quality is never decided by heat input alone. Material science explains why one joint keeps its shape and strength, while another bends, softens, or cracks after cooling. In practical metal joining, the base metal, filler chemistry, and thermal cycle work together. That is why weld strength, distortion, and heat-affected zones must be understood as linked outcomes rather than isolated problems.
Across fabrication, maintenance, construction, transport, and precision assembly, this matters more than ever. Lighter alloys, mixed-material designs, tighter tolerances, and stricter quality standards leave less room for guesswork. For a platform such as GPTWM, which tracks welding practice, metrology, and industrial intelligence, material science is also a decision tool. It connects shop-floor results with wider trends in productivity, safety, and process control.
Why material behavior changes the weld result
Every metal reacts to heat in its own way. That reaction depends on composition, grain structure, thermal conductivity, expansion rate, hardenability, and prior processing history.
Material science gives a practical language for these reactions. It helps explain why carbon steel may harden near the weld, why stainless steel can lose corrosion resistance, and why aluminum often spreads heat fast but still distorts badly.
In simple terms, the weld is not just a melted line. It is a local thermal event that reshapes microstructure, redistributes stress, and changes mechanical behavior in and around the joint.
Three linked zones to watch
The weld metal is the fused region. Its final properties depend on filler selection, dilution, and cooling rate.
The heat-affected zone, or HAZ, does not melt. Even so, it often shows the biggest property shift because heat changes grain size, hardness, and residual stress.
The unaffected base metal keeps its original structure. Yet its restraint level strongly influences distortion and cracking risk during cooling.
What drives weld strength in real production
Strong welds are not created by high penetration alone. They come from a balanced relationship between metallurgy, fit-up, process stability, and service demands.
Material science becomes especially useful when joint failure is unexpected. A weld can look clean on the surface and still fail because the underlying microstructure became too brittle, too soft, or too stressed.
- High-carbon or high-strength steels may form hard, crack-sensitive structures if cooling is too fast.
- Austenitic stainless steels may need controlled heat input to avoid sensitization and loss of corrosion performance.
- Aluminum alloys may lose strength in the HAZ because strengthening precipitates dissolve or coarsen.
- Dissimilar metal joints need close control of filler choice and dilution to prevent weak or brittle interfaces.
This is why procedure settings cannot be copied blindly from one material grade to another. Similar thickness does not mean similar weld behavior.
Strength is also a measurement issue
In many industrial settings, the question is not only whether a weld passed. The better question is whether the measured hardness, distortion, and HAZ width match the part’s service conditions.
That is where precision metrology supports material science. Hardness checks, dimensional inspection, macro-etch review, and thermal monitoring reveal whether the process created the intended structure.
Why distortion starts before the part visibly moves
Distortion is often treated as a layout or fixturing issue. In reality, it starts with uneven expansion and contraction inside the material.
When a weld area heats up, it expands. When it cools, it contracts. If surrounding metal restrains that movement, residual stress develops. Once stress exceeds local resistance, the component bends, twists, or pulls out of tolerance.
Material science helps predict which parts are most sensitive. Thin sections, high thermal expansion alloys, long weld runs, and asymmetric joint designs usually show greater movement.
Usually, less distortion comes from controlled heat, smart weld sequence, and a material-aware setup rather than from brute clamping alone.
Heat-affected zones are small areas with big consequences
The HAZ often decides whether a part performs well in service. This zone can become harder, softer, coarser, or more corrosion-sensitive than both the weld metal and the parent material.
A wide HAZ is not always a defect, but it usually signals more thermal exposure. In many applications, that increases the chance of dimensional change or property loss.
Common HAZ concerns by material family
- Carbon and low-alloy steels may develop hard zones that need preheat or post-weld control.
- Stainless steels may show chromium carbide formation if thermal cycles are poorly controlled.
- Precipitation-hardened aluminum may lose mechanical strength close to the weld.
- Advanced high-strength steels may suffer performance loss if phase balance is disturbed.
From an industry perspective, this is why handheld laser welding, low-heat processes, and smarter parameter monitoring are gaining attention. They can reduce unnecessary HAZ growth when the application allows it.
Where these issues show up across industries
The influence of material science is visible far beyond heavy fabrication. Different sectors care about different failure modes, but the root logic is the same.
In construction equipment and structural repair, toughness and crack resistance often come first. In automotive work, distortion control and repeatability matter because thin sections and tight alignment dominate. In aerospace maintenance, heat input, metallurgy, and traceable inspection are closely linked.
Even in precision tool assemblies, a small HAZ or slight pull can affect fit, calibration, or downstream machining. That aligns with GPTWM’s focus on the last mile of manufacturing, where joining quality directly affects finished performance.
How to apply material science on the shop floor
The best use of material science is practical, not academic. It starts with reading the material condition before striking the arc.
- Confirm the exact base metal grade, thickness, and prior treatment.
- Check whether the filler is compatible with strength, ductility, and corrosion needs.
- Set heat input with the HAZ and distortion target in mind, not only penetration.
- Use preheat, interpass control, or sequencing when the material demands it.
- Measure results after welding, especially hardness, shape change, and visible HAZ behavior.
More importantly, compare actual results with expected service conditions. A weld that is acceptable for static support may fail in vibration, pressure, or corrosive exposure.
Questions worth asking before process changes
If distortion rises, is the root cause heat input, restraint, or a material batch variation?
If cracking appears, did cooling become too fast for the alloy and thickness combination?
If strength drops, did the HAZ lose its intended microstructure even though the weld bead looks sound?
These questions are simple, but they push troubleshooting toward causes that material science can explain clearly.
A practical way to move forward
Better weld decisions usually come from combining welding experience with material science, process data, and inspection feedback. That approach reduces trial and error and makes quality more repeatable across jobs and material types.
A useful next step is to review recurring weld problems by material family rather than by appearance alone. Track where distortion happens, how wide the HAZ becomes, and which combinations of base metal, filler, and heat input deliver stable strength.
When that information is tied to broader intelligence on tools, safety, and metrology, the welding process becomes easier to judge with confidence. In that sense, material science is not just background knowledge. It is a practical framework for stronger joints, better dimensional control, and smarter industrial decisions.
Related News
How Procurement Teams Can Map the Industrial Value Chain to Reduce Supply Risk
Industrial value chain procurement helps teams map hidden dependencies, qualify resilient sources, and reduce supply risk before disruptions stop production.
How Specification-Driven Articles Improve Precision Measurement System Selection
Specification-oriented articles precision measurement guidance helps teams compare accuracy, repeatability, environment, and data needs to select reliable systems with confidence.
How to Evaluate a Technology Integration Service Provider for Complex Projects
Technology integration service provider selection guide: evaluate interface ownership, delivery discipline, scalable architecture, and risk control for complex projects.
How Battery, Torque, and Duty Cycle Affect Cordless Power Tool Efficiency
Cordless power tool efficiency depends on battery output, torque, and duty cycle. Learn how to match tools to demanding jobs for stronger runtime and productivity.
Product Comparison Resources for Component Compatibility and Lifecycle Risk
Product comparison resources for components: evaluate compatibility, interfaces, service support, and lifecycle risk to reduce downtime, avoid redesigns, and make confident sourcing decisions.
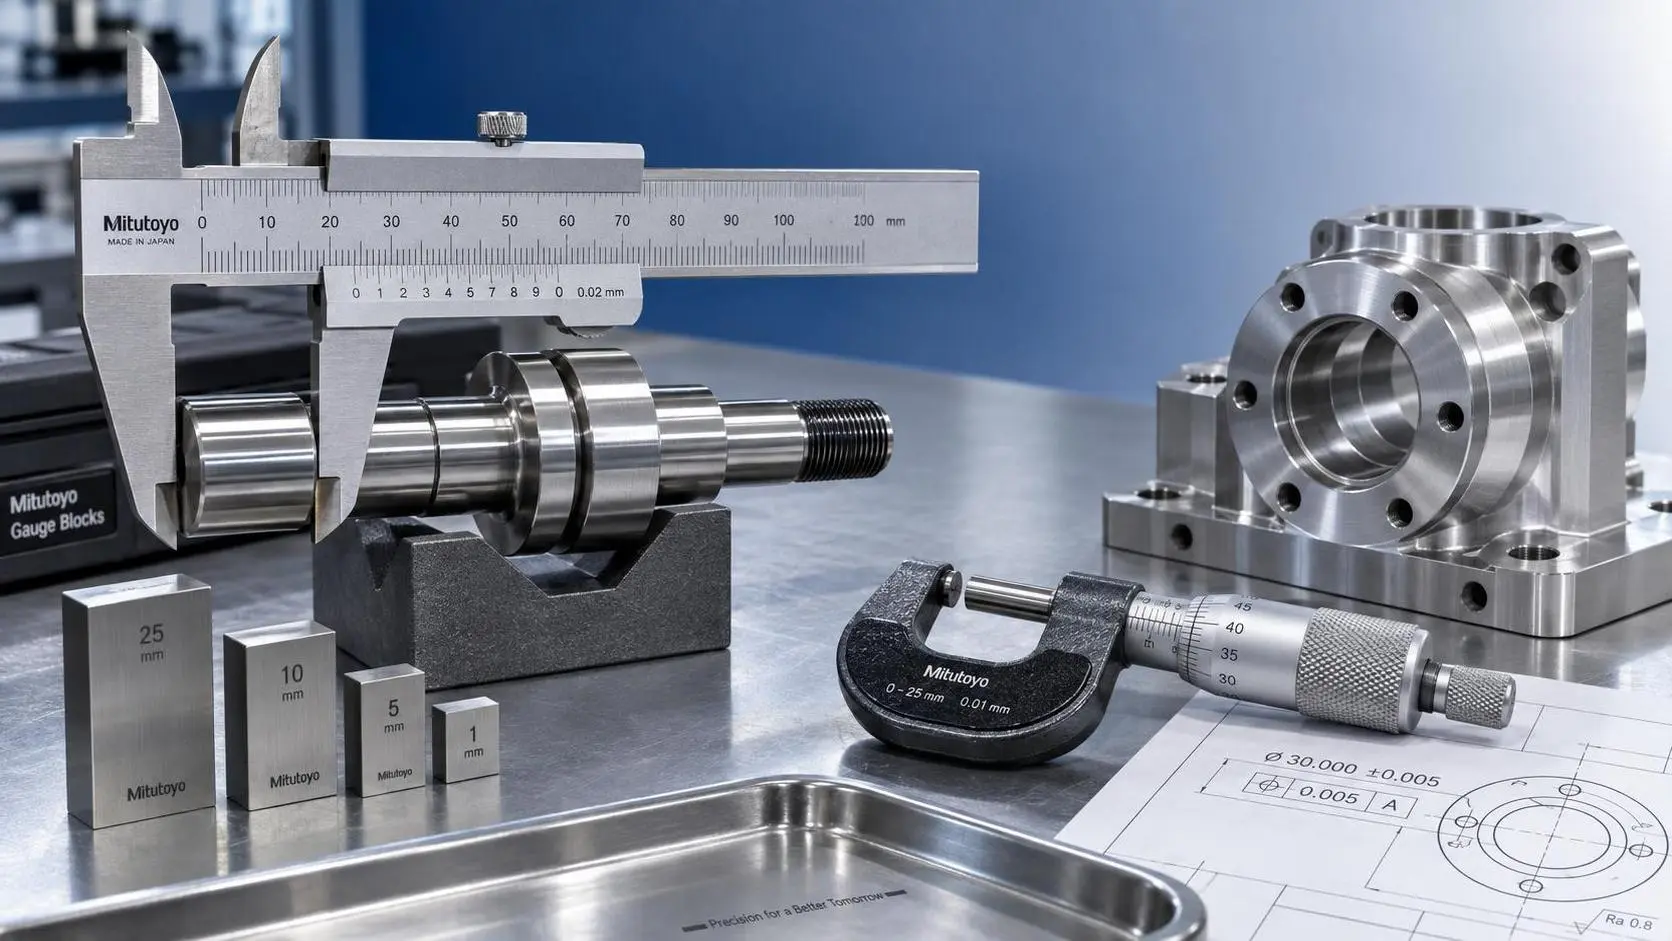
How to Select Vernier Precision Calipers for Tight-Tolerance Machining Inspection
Vernier precision calipers for tight-tolerance machining: learn how to select the right range, jaw design, accuracy, and verification process for reliable inspection.
Product Comparison Resources in Europe: How Buyers Can Verify Specs and Suppliers
Product comparison resources Europe: learn how to verify industrial specs, compliance claims, supplier credibility, and delivery risk for smarter purchasing decisions.
How to Evaluate an Industrial Metrology Solution Manufacturer for Production Use
Industrial metrology solution manufacturer evaluation guide for production: compare accuracy, traceability, automation, software, service, and acceptance testing to reduce risk.
Which ISO Standards Matter Most for Precision Engineering Quality Control?
Precision engineering ISO standards explained: discover how ISO 9001, ISO/IEC 17025, ISO 10012, GPS, and ISO 3834 strengthen quality control, traceability, and compliance.
Related News
- 00
0000-00
How Specification-Driven Articles Improve Precision Measurement System Selection - 00
0000-00
Product Comparison Resources for Component Compatibility and Lifecycle Risk - 00
0000-00
Which ISO Standards Matter Most for Precision Engineering Quality Control? - 00
0000-00
Selecting Metal Joining Methods for Aluminum-to-Steel Assemblies - 00
0000-00
How to Evaluate Industrial Manufacturing Systems for Throughput, Flexibility, and ROI
Prof. Marcus Chen
Weekly Insights
Stay ahead with our curated technology reports delivered every Monday.